 EN

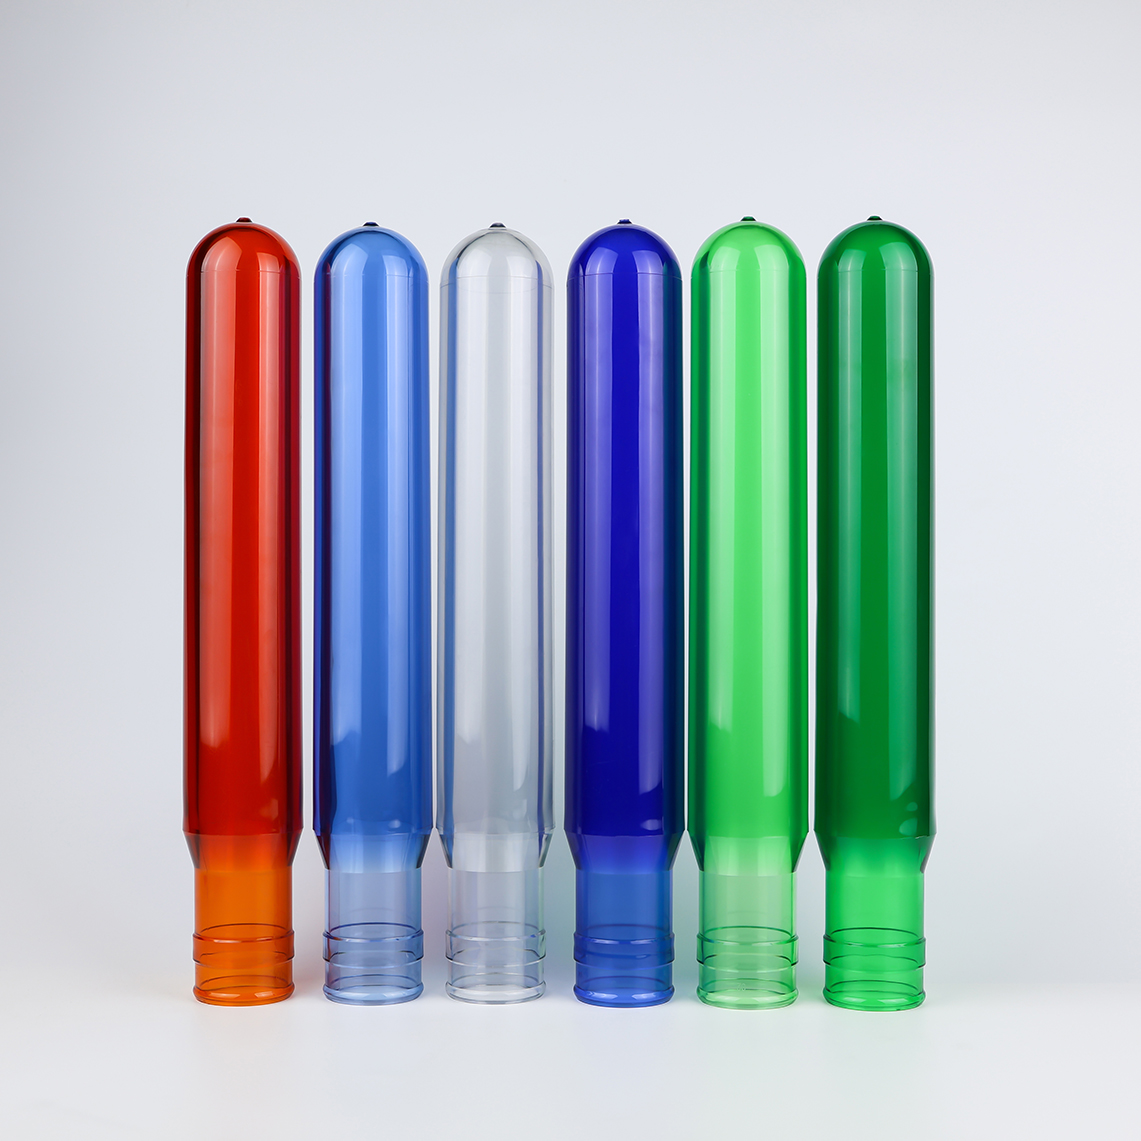
When beverage manufacturers and brand owners evaluate packaging quality, one often overlooked but decisive factor is how the bottle preform is engineered at the initial mold design stage. Preform design choices — including wall thickness taper, gate geometry, virgin resin selection, and tight neck finish tolerances — directly decide whether the final blown bottle delivers crystal transparency and a smooth, premium surface finish expected by retailers and end consumers. This relationship matters greatly for teams working on drinking water, still beverage and carbonated drink packaging.
A PET bottle preform is far more than a simple resin blank for stretch blow molding. Every geometric feature and material parameter of the preform will shape optical performance, structural stability and surface quality of the finished bottle. This guide breaks down how key preform design variables influence bottle clarity and surface finish, helping procurement specialists, packaging engineers and brand teams make better decisions on preform specification and supplier selection. Our factory supports custom mold development to tune these design factors for consistent visual quality across mass production.
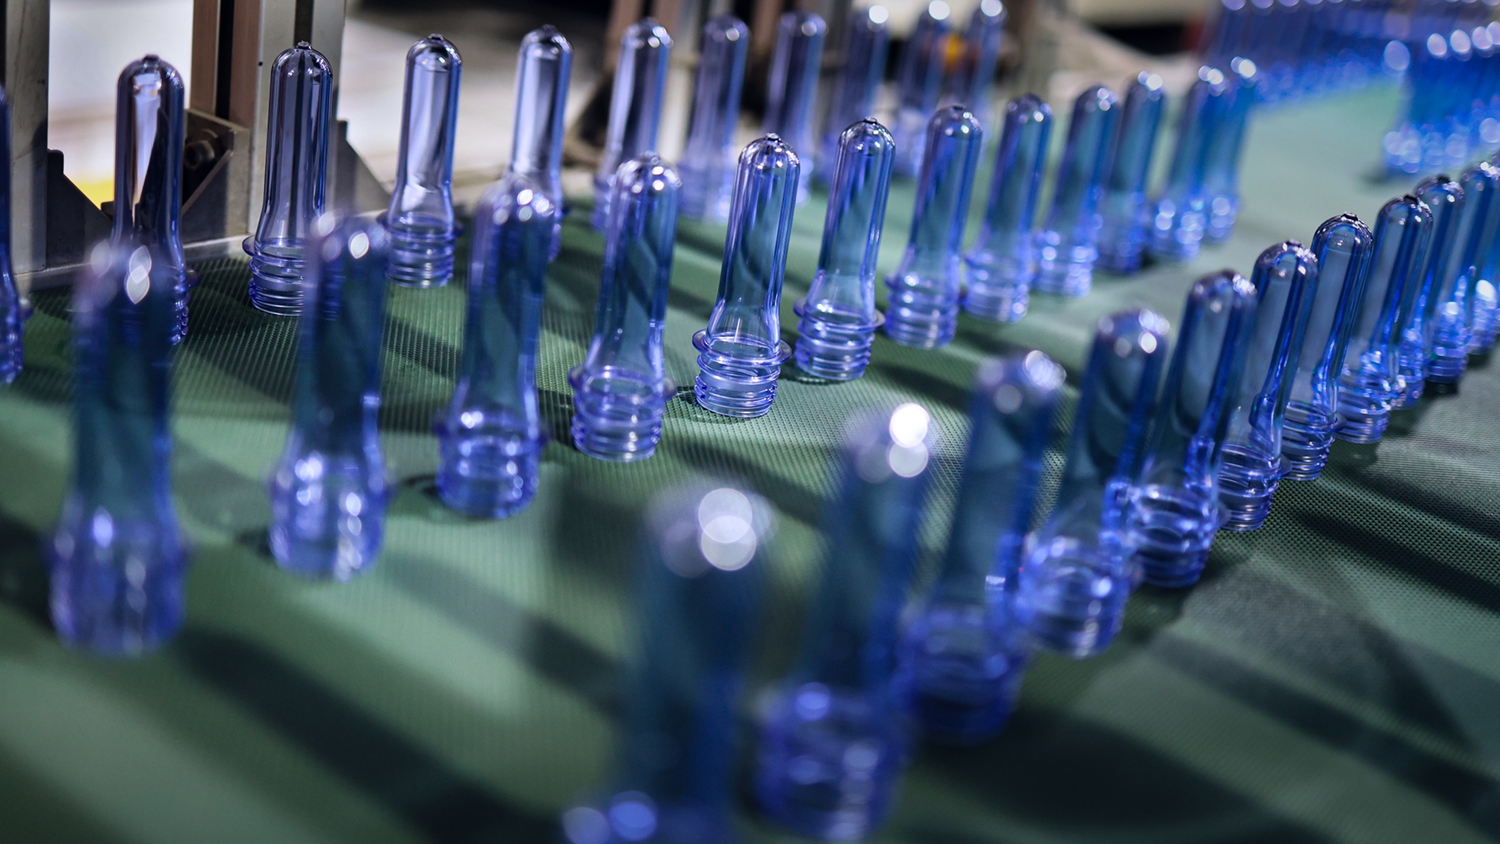
The Role of PET Resin Quality in Optical Clarity
Intrinsic Viscosity and Its Optical Consequences
Bottle clarity starts at the molecular level, governed by the intrinsic viscosity (IV) of the PET resin used for injection molding. IV reflects polymer chain length and controls material behavior during injection and stretch blow molding. Preforms made with stable IV within 0.72–0.84 dL/g for beverage packaging stretch evenly, lowering risks of stress whitening and haze on finished bottles.
If IV is too low, polymer chains cannot orient uniformly during biaxial stretching, creating thin spots and uneven transparency. Too high IV restricts resin flow inside the mold cavity, raising shear stress and leaving visible streaks or cloudy areas on preform walls. Reliable preform manufacturers lock resin IV inside a narrow specification window to maintain stable optical quality batch by batch.
Acetaldehyde content is another resin-linked indicator for visual quality. While it mainly impacts beverage flavor and odor, excessive acetaldehyde usually signals thermal degradation during molding. This degradation often comes with yellow tint, haze or tiny surface defects that remain visible after blow molding. Our food-grade production follows ISO22000 standards to control thermal exposure and reduce such defects.
Moisture Content and Crystallinity Control
PET absorbs moisture easily. Any residual moisture during preform injection triggers hydrolytic degradation of polymer chains, resulting in reduced clarity, cloudy surfaces and milky frosted texture on blown bottles. Fully drying resin down to below 50 ppm moisture is a mandatory quality step for consistent clear preform output.
Crystallinity management is equally critical. Amorphous PET stays transparent; crystallization turns PET opaque or whitish. Improper mold cooling or long residence time inside the injection barrel will create crystalline spots, commonly near the gate and preform base. These opaque zones cannot be fixed in later blow molding and will show as permanent cloudy patches on finished bottles. Strict temperature monitoring in our injection workshop minimizes unwanted crystallinity.
Wall Thickness Distribution and Its Effect on Clarity
Uniform Stretching as the Foundation of Transparency
Preform wall taper and thickness distribution are core design factors deciding final bottle clarity. If the preform wall profile does not match the target blow mold geometry, stretching will become uneven. Over-stretched areas turn overly thin and develop haze from orientation stress, while under-stretched sections stay thick and may show opaque or blueish tint under light.
Axial and hoop stretch ratios must be calculated precisely in preform design. Standard beverage bottles need balanced biaxial orientation at 2.5–4.5x in both directions, which requires gradual wall thinning from the neck toward the base. This tapered profile comes from precision mold cavity design and separates high-quality custom preforms from generic commodity options.
Consistent bottle clarity is achieved when molecular orientation is balanced across the whole bottle wall. Design teams run blow simulation and physical sampling, iteratively adjusting preform wall profiles to reach the target optical effect. Our mold team provides this simulation & sampling service for custom preform projects.
Gate Design and Base Clarity
The injection gate is where molten PET enters the cavity, and its design strongly impacts base clarity and overall preform quality. Improper gate size or placement brings extra shear heat at the injection point, triggering local thermal degradation and leaving yellow or brown tint on the bottle base after blowing.
Gate vestige is the small leftover mark after de-gating. High-quality preform tooling keeps vestiges flat or slightly recessed, avoiding sharp bumps that break optical uniformity or create stress points for carbonated beverage bottles. Rough, oversized gate marks cause base haze and become a frequent rejection reason for premium beverage brands.
Modern hot runner valve gate systems greatly ease these issues for mass production. Even so, gate geometry must be optimized for each preform weight grade and resin type to keep stable base clarity over millions of molding cycles.
Neck Finish Design and Surface Smoothness
Thread Geometry and Dimensional Tolerance
The neck finish is the most tightly controlled section of a preform; it does not stretch during blow molding and its shape is fully defined by the mold. Thread profile, neck diameter, sealing face and transfer ring dimensions are held within tight tolerances, often ±0.05 mm, to guarantee stable cap torque, leak-proof sealing and clean visual appearance on bottle shoulders and necks.
Preforms with out-of-spec neck finishes produce bottles that fail leakage tests, show deformed threads or uneven sealing surfaces. These defects matter a lot for mineral water and carbonated drinks, where the neck-shoulder area is highly visible to buyers and sealing reliability is essential for food safety. We produce standard neck sizes including 28mm, 30mm, 38mm, 45mm, 48mm and 55mm, and support custom neck structure design.
The widely adopted 28mm 1881 neck standard balances material usage, sealing stability and visual performance for water and beverage packaging. Preforms built to this standard require stable dimensional control to deliver consistent finish quality on customers’ blow lines.
Surface Finish of the Preform Cavity
The polishing grade of mold cavity surfaces transfers directly to the outer surface of preforms and blown bottles. Mirror-polished cavities produce glossy preforms with high light transmission and low surface haze.
Scratches, pits and tool marks inside cavities will replicate on every preform from that mold. Progressive mold wear gradually ruins surface quality and raises cosmetic rejection rates. Planned mold inspection, cleaning and repolishing are essential to maintain clarity in high-volume runs.
Mold cavity contamination from degraded resin, release agent residue or fine particles creates pinholes, flow lines or dull patches that remain visible after blowing. This risk is especially critical for premium bottled water and specialty beverages with strict visual requirements.
Preform Weight and Geometry Relative to Final Bottle Requirements
Matching Preform Weight to Bottle Volume and Shape
Selecting the right preform weight for your bottle size and shape is key for both clarity and mechanical performance. An under-weight preform will over-stretch, creating thin, hazy and fragile zones. An overweight preform stretches insufficiently, forming thick, semi-opaque walls with reduced gloss.
Common 500ml mineral water bottles usually use 14g–20g preforms; 1.5L+ large bottles often need 30g–46g preforms depending on wall strength and bottle complexity. These weight ranges are derived from validated stretch ratios that deliver balanced orientation and ideal transparency.
The length-to-diameter ratio of the preform body also affects heating uniformity during reheat blow molding. Overlong, narrow preforms paired with short, wide bottle shapes easily create hot or cold spots, leading to irregular blow results and inconsistent clarity. Preform geometry should be co-designed together with blow mold geometry at the beginning of a packaging project.
The Impact of Lightweight Designs on Finish Quality
Lightweighting is a mainstream trend for PET packaging to cut raw material cost and support sustainability goals. However, simply reducing preform gram weight without redesigning wall taper and neck geometry hurts clarity and surface finish. Thinner walls leave far smaller tolerance for process fluctuation; tiny shifts in melt temperature, cooling cycle or blow pressure create obvious visual differences.
Successful lightweight preform design is holistic: it optimizes stretch ratio, orientation balance, neck reinforcement and base geometry together. Blind weight reduction without geometry adjustment pushes up reject rates and unstable optical quality. Reliable lightweight preforms come from simulation, prototype testing and production trials, not just cutting grams.
Process Parameters That Amplify or Undermine Preform Design
Injection Molding Conditions and Their Optical Effect
Even well-designed preforms lose clarity if injection parameters drift. Melt temperature, injection speed, packing pressure and cooling time all change optical performance. Overheating triggers thermal degradation and yellowing; insufficient cooling causes crystalline haze; unstable packing pressure brings inconsistent wall thickness and sink marks that turn into visible defects after blowing.
Process repeatability is just as important as design quality when choosing a preform supplier. Multi-cavity molds running at high speed must keep identical conditions on every cavity so all preforms share the same dimension and visual quality. Cavity variation is a well-known pain point, solved by precision tooling and continuous process monitoring in our workshop.
Reheat and Blow Conditions in the Context of Preform Design
The preform is an intermediate part; its final visual quality heavily depends on reheat stretch blow molding settings. A preform optimized for a certain heating lamp layout, heating duration and stretch rod profile only performs best under matched downstream parameters. Switching blow equipment or adjusting process recipes without re-evaluating preform design is a common source of clarity defects.
Temperature distribution during reheating matters most. The preform base needs cooler conditions to avoid crystallization, while shoulder zones demand precise heating for even material flow into the bottle shoulder and neck transition. Preforms engineered with this thermal gradient in mind deliver cleaner, more uniform bottles than generic alternatives under the same blow setup.
FAQ
How does wall thickness in a bottle preform affect the final bottle's transparency?
Wall thickness distribution controls material stretch uniformity during blow molding. Uneven stretching creates inconsistent molecular orientation, leading to optical variation — some areas stay clear while others turn hazy or opaque. A well-tapered preform wall supports balanced biaxial stretching and uniform orientation, delivering steady clarity across the whole bottle.
Why does the gate area of a bottle preform sometimes appear different from the rest of the bottle?
The gate region receives the highest shear heat in injection molding. Poor gate design or long resin residence time causes local degradation, yellowing or crystallization. This becomes a tinted or cloudy spot at the bottle base after blowing. Optimized gate geometry, valve gate technology and controlled mold temperature reduce this defect and keep base clarity consistent with the bottle body.
Can changing bottle preform weight affect surface finish quality?
Yes, significantly. Preform weight mismatch alters stretch ratio and breaks uniform orientation. An overweight preform creates thick, low-gloss walls with light haze; an underweight preform produces over-stretched walls vulnerable to stress whitening. Matching preform gram weight to your bottle mold is essential for stable surface finish and clarity.
What is the most common cause of cloudiness in a PET bottle, traced back to the bottle preform stage?
The top root cause is moisture inside PET resin during injection, which leads to hydrolytic degradation and milky haze that cannot be fixed in blow molding. The second major cause is thermal degradation from excessive melt temperature or long barrel residence time, creating yellowish cloudy defects. Both risks must be controlled at the preform manufacturer’s production stage.
Can custom mold polishing and gate design improve preform clarity for premium packaging?
Absolutely. Custom cavity polishing, optimized gate layout and targeted cooling channel design are effective ways to reduce haze, gate marks and surface blemishes. Our mold-making team tunes these features together with your clarity requirements, suitable for premium drinking water and branded beverage packaging projects.
Table of Contents
- The Role of PET Resin Quality in Optical Clarity
- Wall Thickness Distribution and Its Effect on Clarity
- Neck Finish Design and Surface Smoothness
- Preform Weight and Geometry Relative to Final Bottle Requirements
- Process Parameters That Amplify or Undermine Preform Design
-
FAQ
- How does wall thickness in a bottle preform affect the final bottle's transparency?
- Why does the gate area of a bottle preform sometimes appear different from the rest of the bottle?
- Can changing bottle preform weight affect surface finish quality?
- What is the most common cause of cloudiness in a PET bottle, traced back to the bottle preform stage?
- Can custom mold polishing and gate design improve preform clarity for premium packaging?
